Solar System for Factory
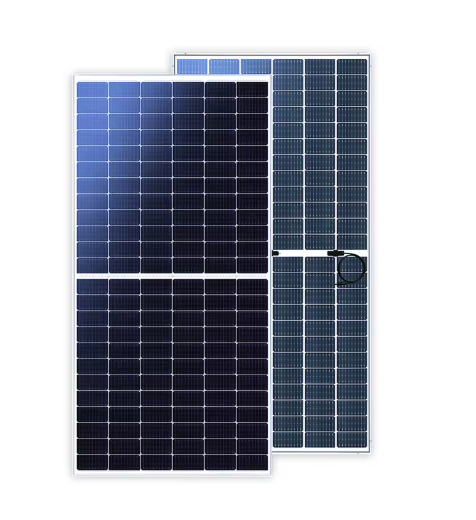
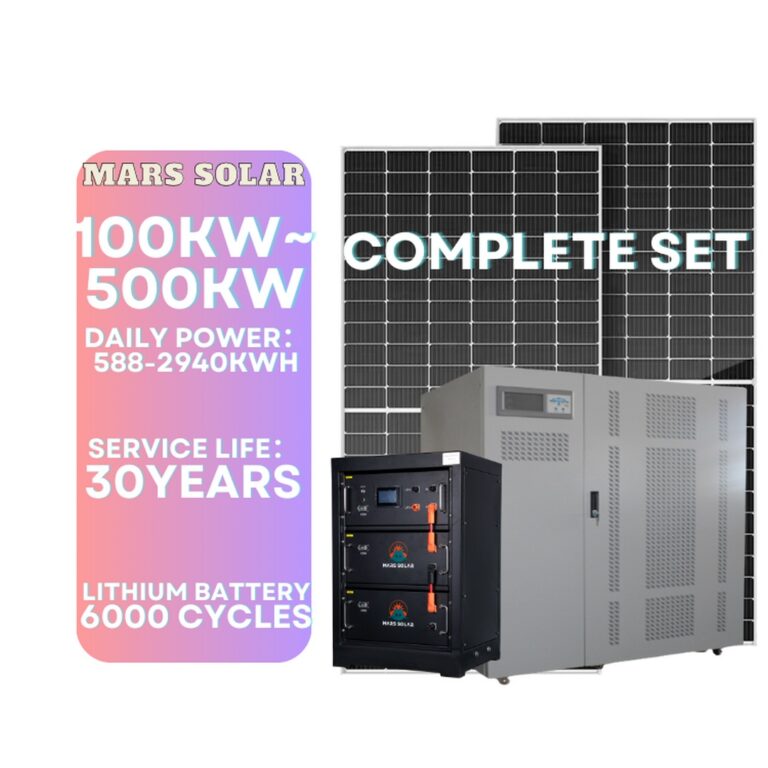
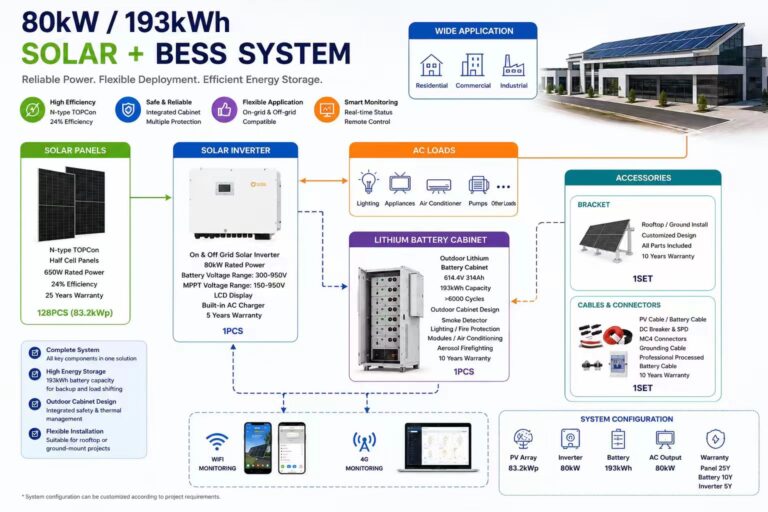
Complete package includes: high-efficiency solar panels, durable solar brackets, long-cycle solar batteries (6,000+ charge-discharge cycles at 80% DoD), solar inverter with MPPT controller (conversion efficiency ≥95%), high-temperature resistant cables, and MC4 connectors.
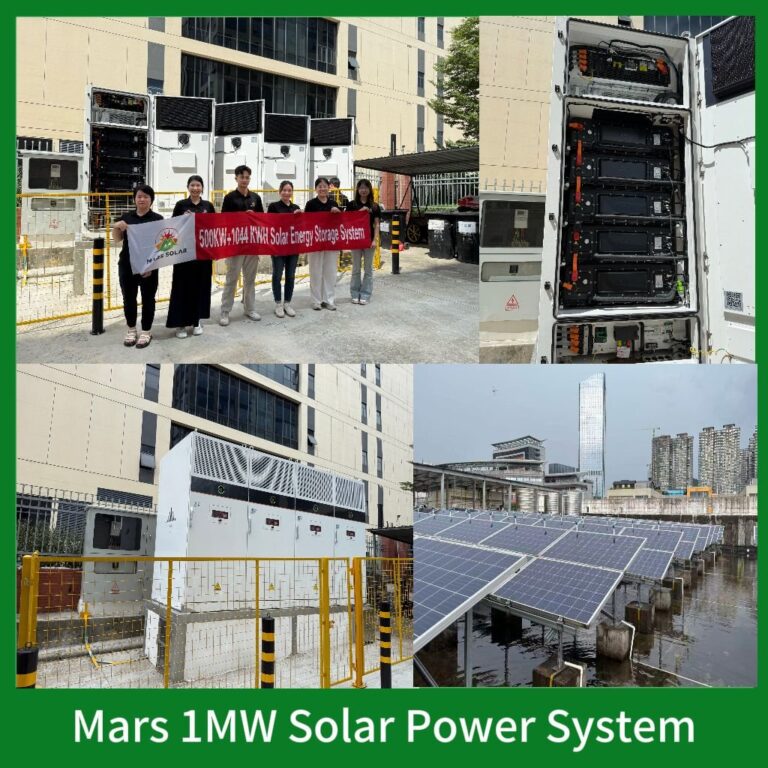
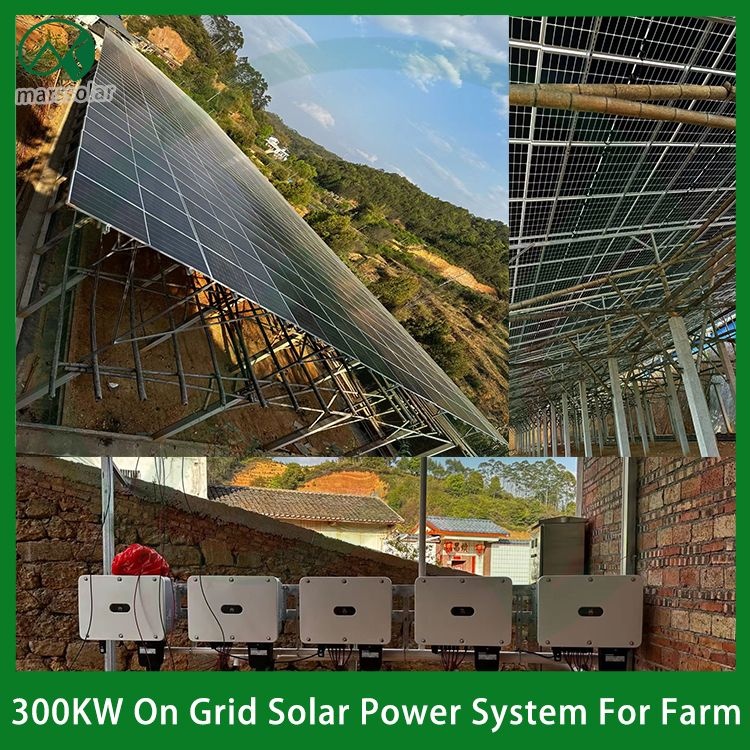
Our hot-selling solar system for factory ranges from 100KW to 2MW, featuring DC 110V/220V /380V to AC 110V~480V wide voltage output, suitable for medium-large factories and manufacturing facilities. Fully customizable to your factory’s energy needs (capacity, voltage, installation layout).
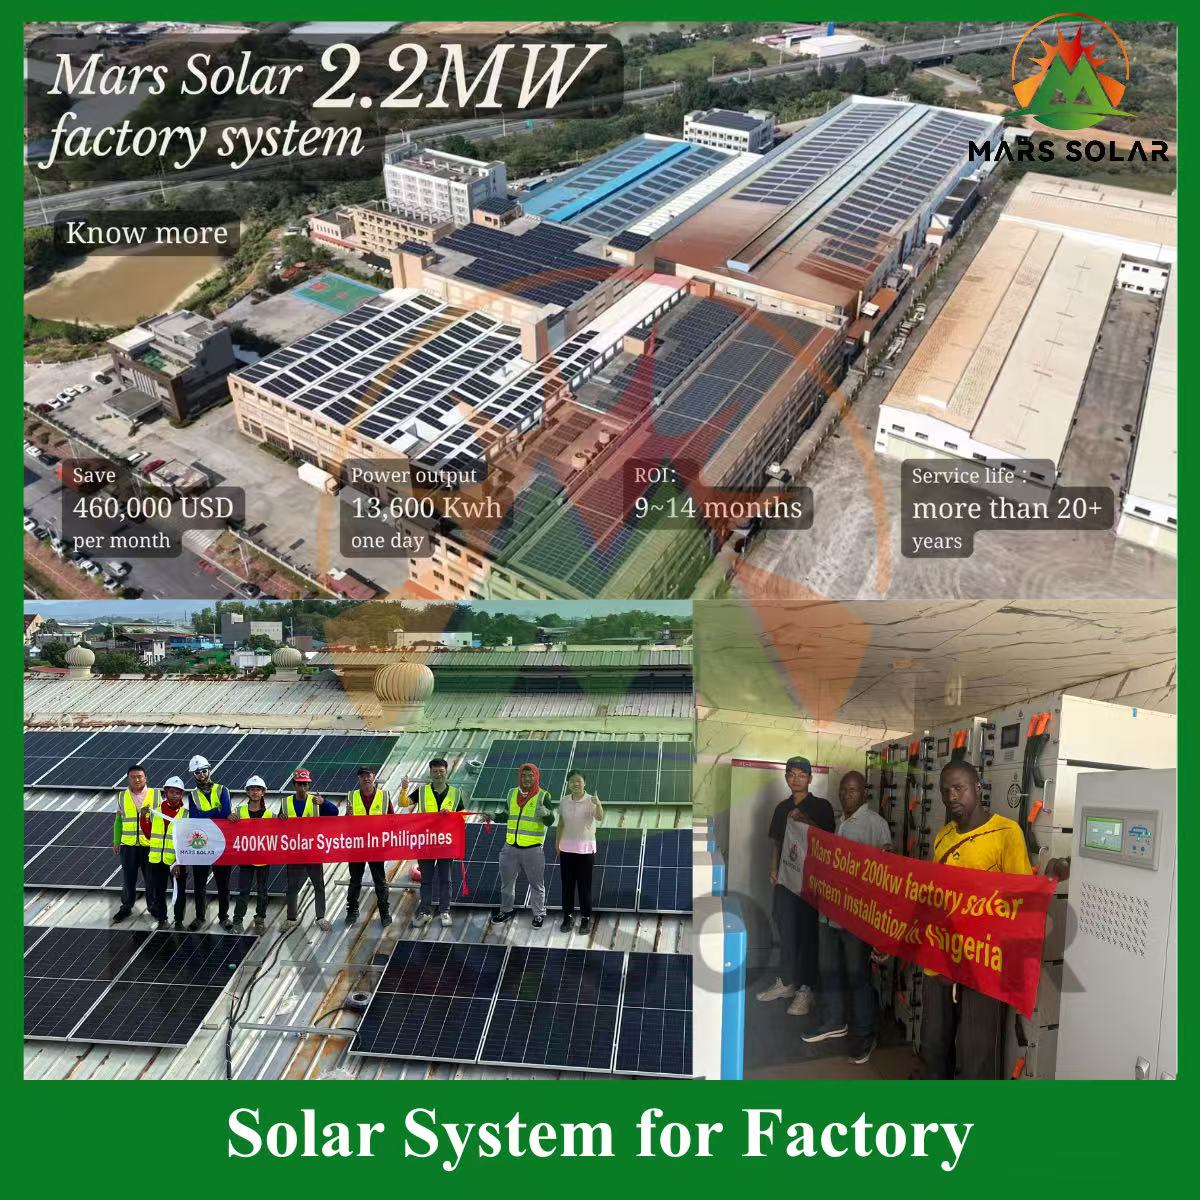
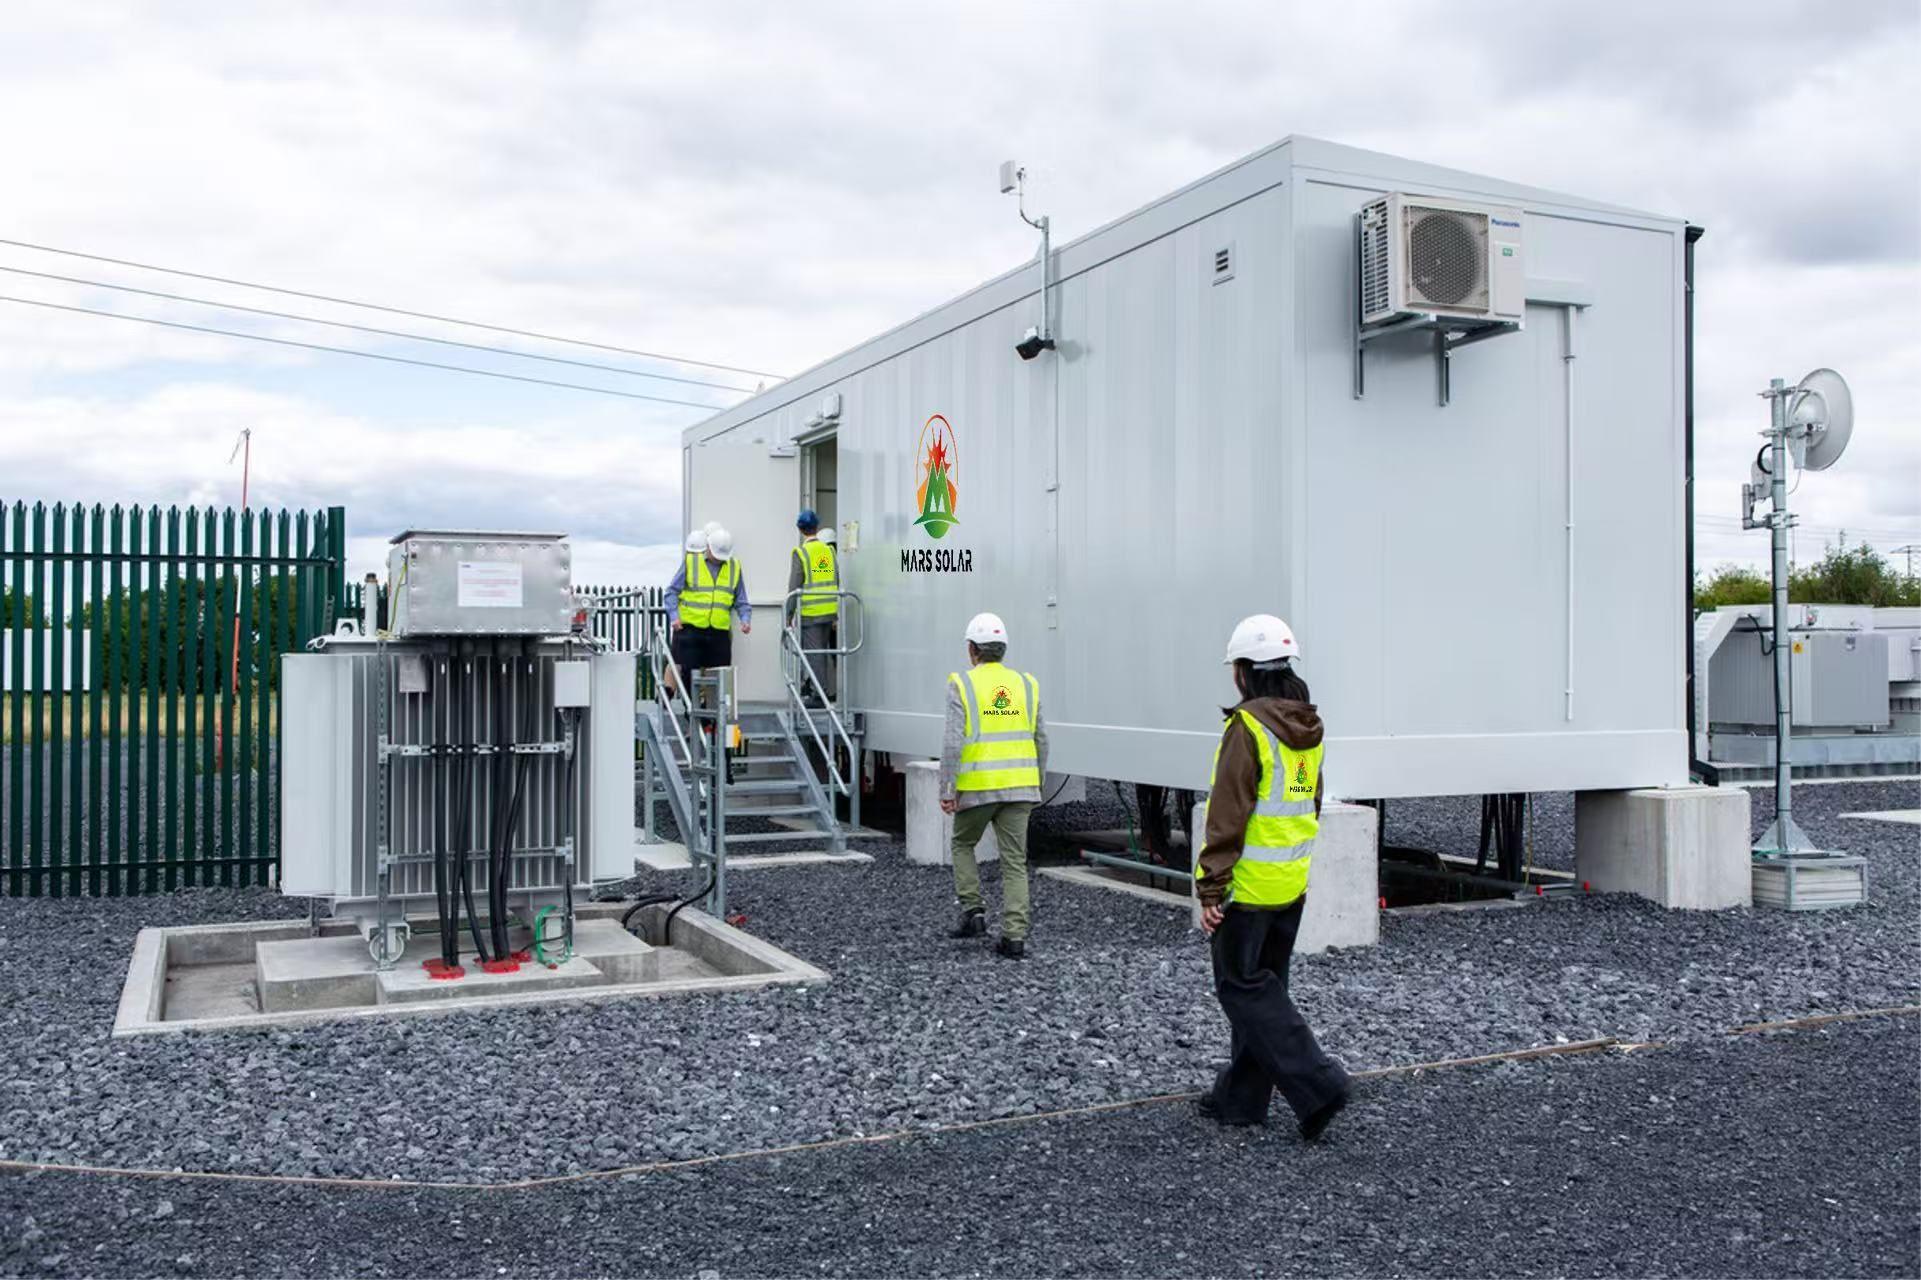
For a real-world reference, see how we engineered a solar system for an electroplating factory — 2 MW, $26,500/month savings, 11-month payback.
Product Specification
AC: 110V~480V
Share as:
Video Showcase
Advantages
Parameters
MOQ: 1 set,Accept OEM &ODM
Certificate: TUV, ETL, ISO, CE, RoHS
Payment: T/T, L/C, Paypal, Western Union
System Equipment List

What a Solar System for Factory Must Deliver
A solar system for factory has to do more than cut an electricity bill - it must protect production. Motor starts, welding sets, compressors and CNC lines create surge loads and power-quality events that a domestic system cannot absorb. A solar system for factory is designed around the load profile of the plant, not around a nameplate rating.
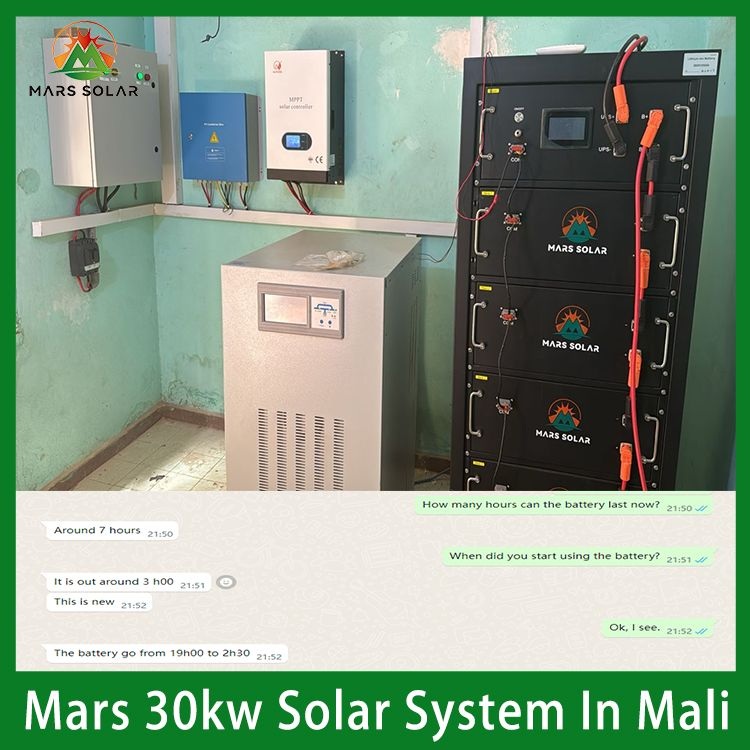
In Nigeria, Ghana and Kenya, where grid interruptions stop a shift mid-run, the storage component matters as much as the PV array. Our electroplating factory solar system case explains how that is engineered.
Sizing PV and Storage for Industrial Loads
We start with 7 to 14 days of logged consumption, split base load from shift peaks, and size the PV array on daytime energy while sizing the battery on the evening block. A plant consuming 900kWh a day with a 400kWh daytime share needs roughly 100kWp of PV plus a storage bank covering the remaining 500kWh.
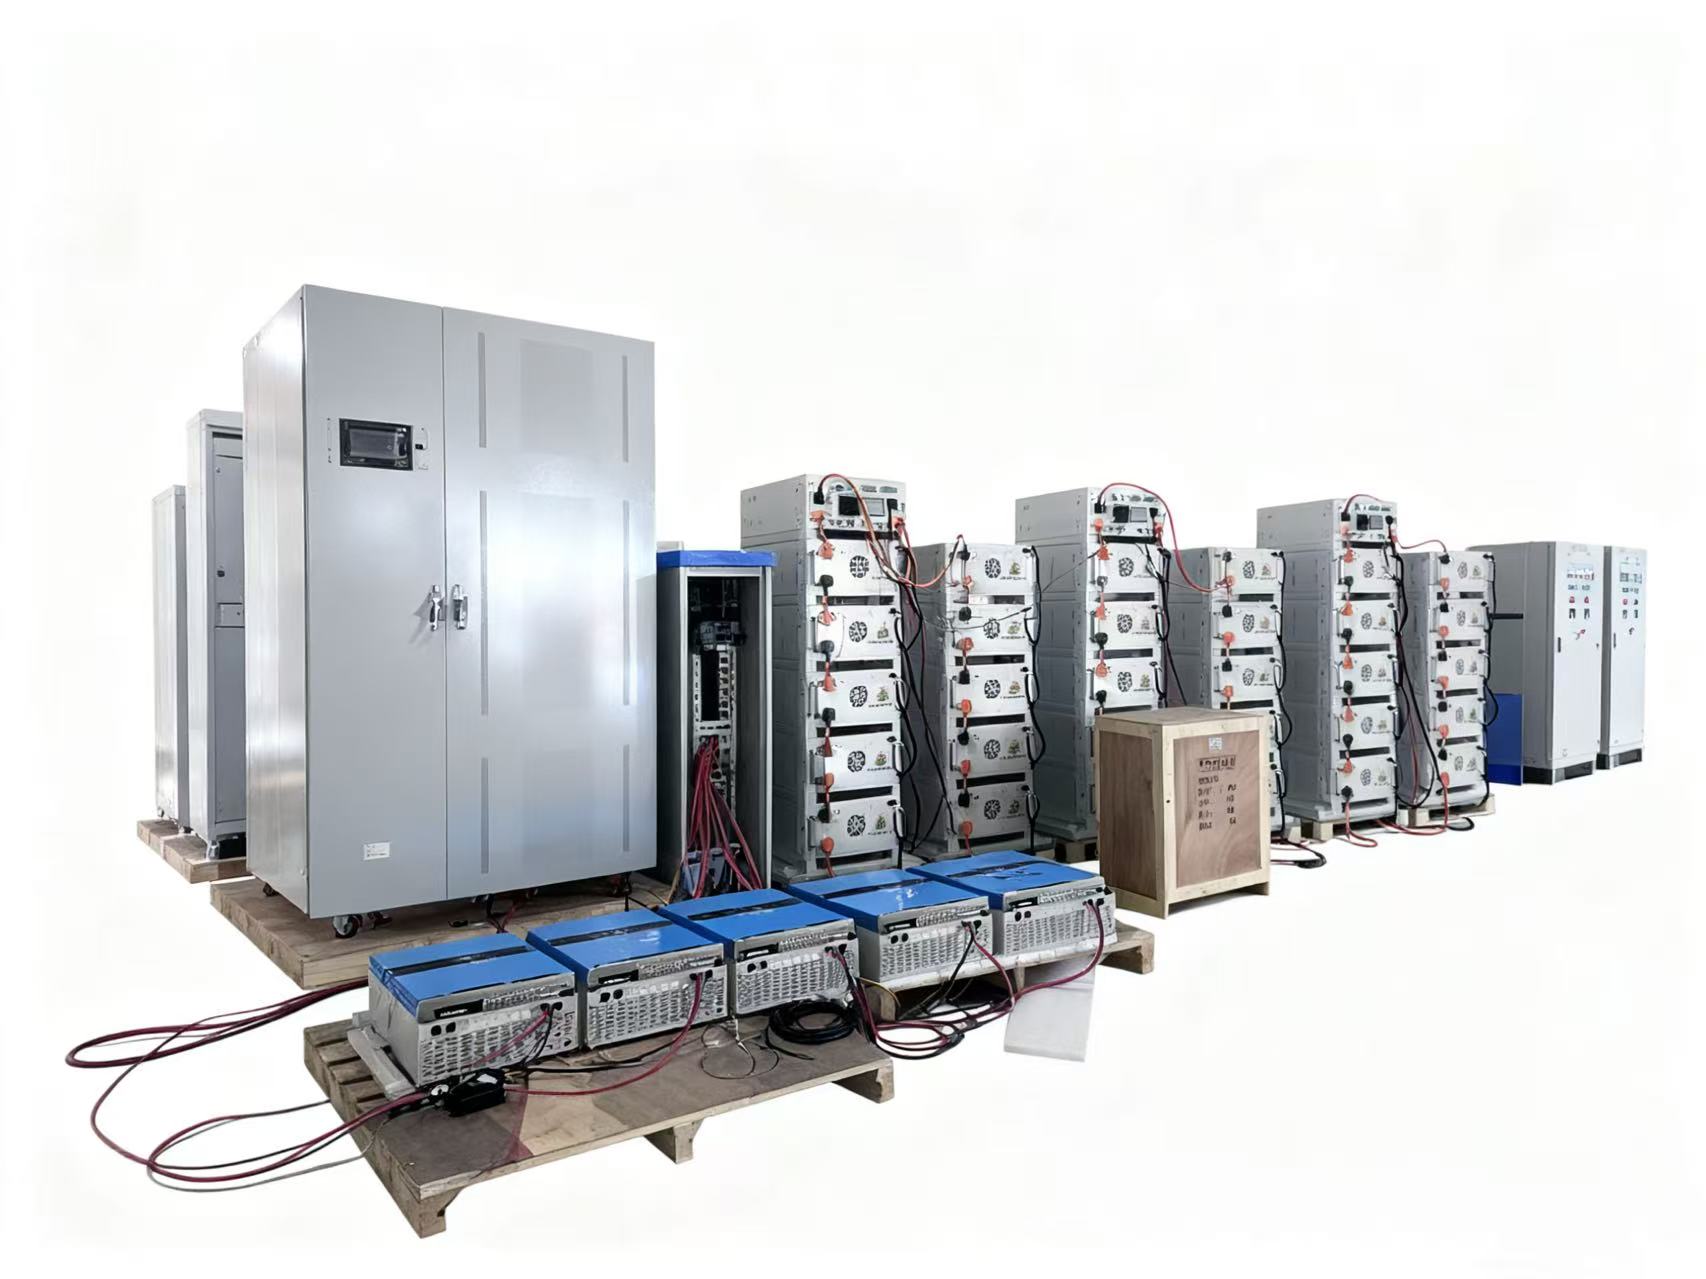
Inverter selection follows the surge profile. Three-phase machinery with 3x inrush needs a bidirectional inverter rated for that surge, which is why we specify an 125kW BESS rather than stacking single-phase units.
Send the motor list and twelve months of bills, and your solar system for factory proposal comes back with a sized PV array, inverter rating and battery capacity.
What a Solar System for Factory Includes
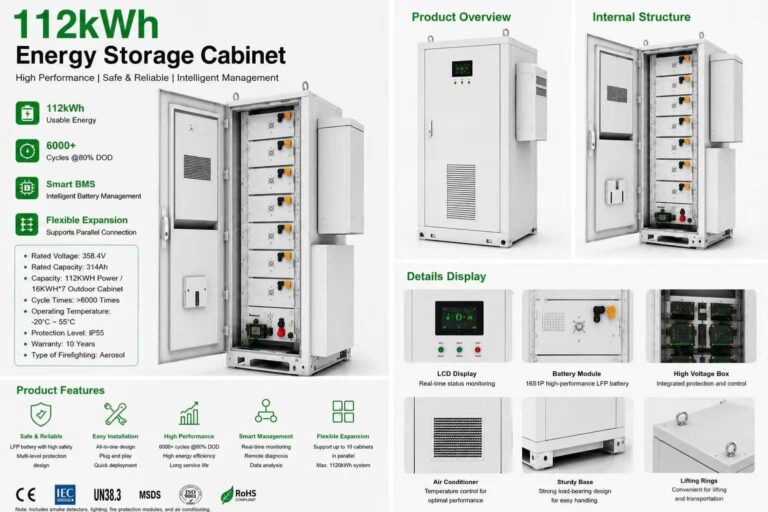
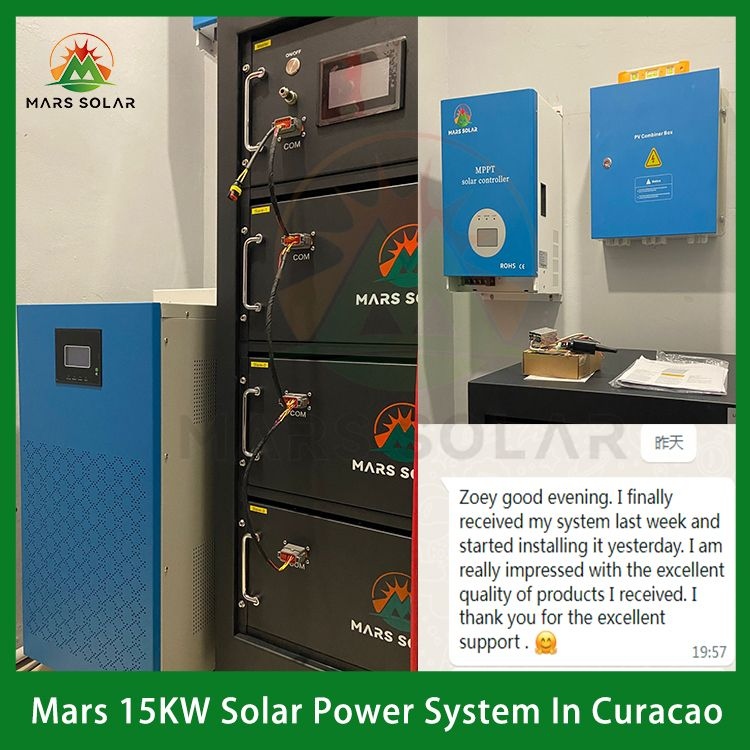
A complete solar system for factory from Mars Solar includes PV modules, mounting structure, DC and AC protection, hybrid or bidirectional inverters, LiFePO4 storage, cable, MC4 connectors and a monitoring gateway. Everything is matched and factory-tested as one system.
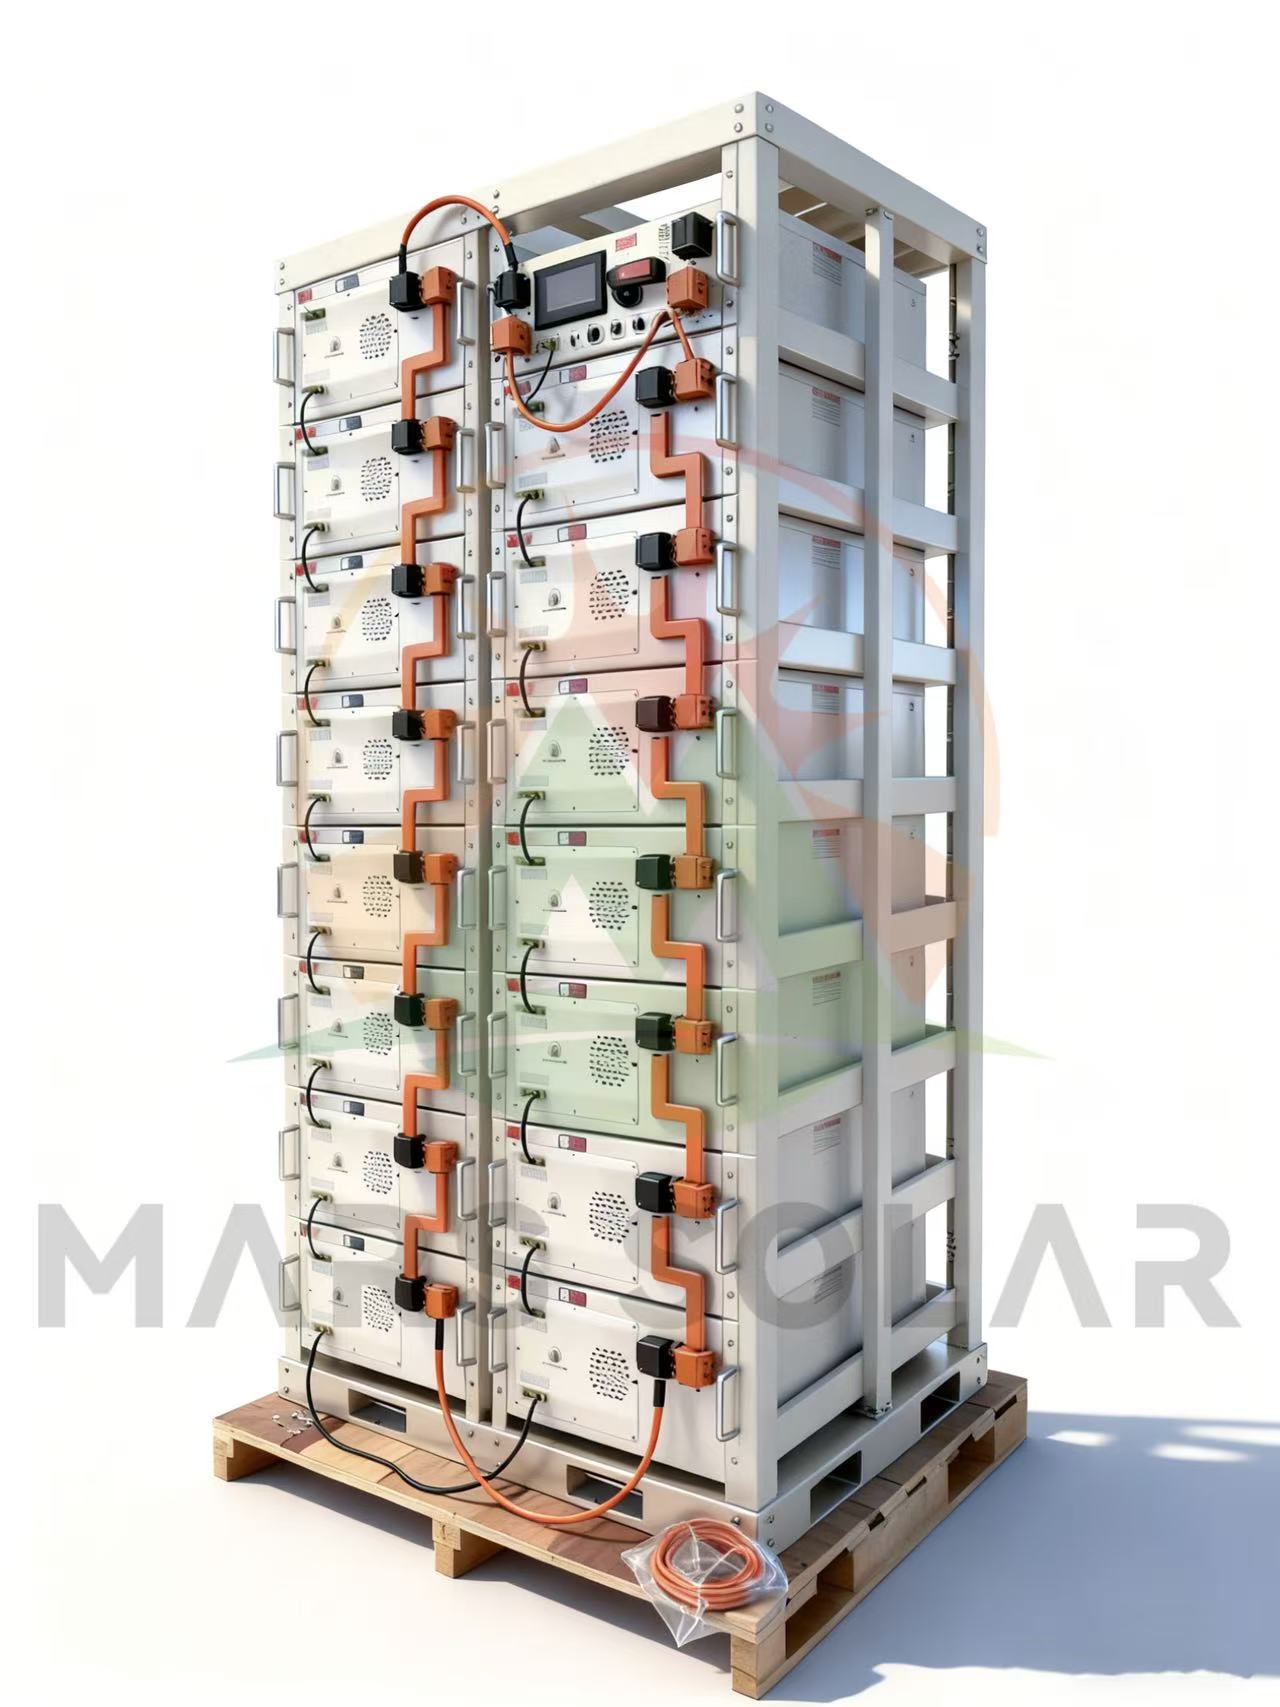
Storage modules are rack-mounted for serviceability, as shown on our rack mounted energy storage battery page. For plants with a heavy overnight load, see the 2MW factory solar case.
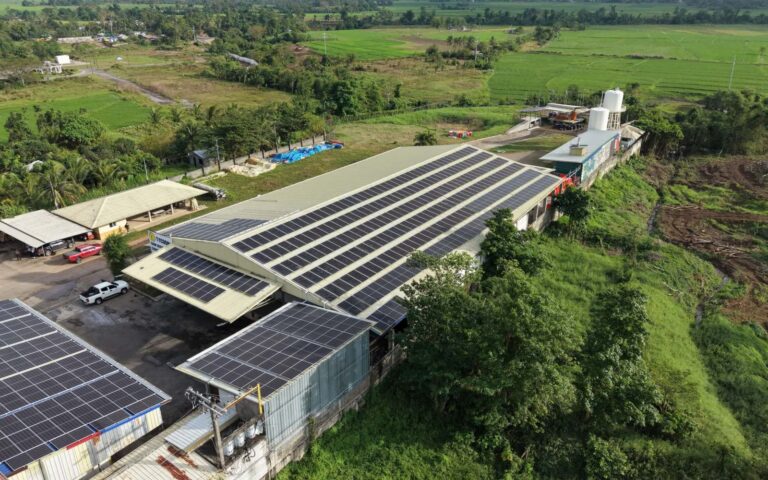
A solar system for factory rooftops and yards is only as good as the load data behind it; every solar system for factory we ship is sized from logged consumption, not from a template.
Buying a Solar System for Factory Direct
Mars Solar exports industrial systems directly, so a solar system for factory is priced at factory level without distributor margin. Systems are certified to CE, RoHS, TUV and ISO standards, with a 10-year battery warranty and 5-year inverter warranty.
Model the investment with our storage cost guide, and see commissioning practice in our Sudan microgrid build.
Industrial energy is the largest single category of global demand. The U.S. Department of Energy's Solar Energy Technologies Office explains how on-site generation cuts both cost and carbon for manufacturing - a solar system for factory is a cost-reduction measure before it is an environmental one.
Frequently Asked Questions
How is a solar system for factory sized?
We start with 7 to 14 days of logged consumption, split base load from shift peaks, and size the PV array on daytime energy while sizing the battery on the evening block. A plant consuming 900kWh a day with a 400kWh daytime share needs roughly 100kWp of PV plus a storage bank covering the remaining 500kWh.
What should buyers check before ordering a solar system for factory?
Mars Solar exports industrial systems directly, so a solar system for factory is priced at factory level without distributor margin. Systems are certified to CE, RoHS, TUV and ISO standards, with a 10-year battery warranty and 5-year inverter warranty.
A Day on Site: Factory Load and System Operation
Worked example for sizing discussion, not a project measurement. A plant consuming about 900 kWh a day with a 400 kWh daytime share, served by 100 kWp of PV (about 450 kWh a day) and a storage bank carrying the remaining 500 kWh outside the solar window.
| Time | Main loads | Average kW | kWh in block | Supply and battery |
|---|---|---|---|---|
| 22:00–06:00 | Continuous process, finished-goods cold store, security and yard lighting | 42 | 336 | Battery carries the whole night block |
| 06:00–08:00 | Shift start-up: compressors, motor inrush, welding sets | 30 (about 3× on start) | 60 | PV plus battery; the battery absorbs the start-up surge |
| 08:00–12:00 | Morning shift at full production | 37 | 150 | PV direct |
| 12:00–14:00 | Break and shift handover, base load only | 20 | 40 | PV direct; surplus charges the battery |
| 14:00–18:00 | Second shift at full production | 38 | 150 | PV direct; battery covers the difference |
| 18:00–22:00 | Second-shift tail: finishing lines, packing, yard lighting | 40 | 160 | Battery carries the block |
Reading the day: about 385 kWh is consumed at the moment it is generated, and roughly 500 kWh falls outside the solar window and is carried by the storage bank, with the grid or a generator as backstop. The 65 kWh of midday surplus is captured rather than exported. The 06:00–08:00 block is the hard one — motor inrush is a power problem measured in kW, not an energy problem measured in kWh, so it sets the inverter rating rather than the battery size.
kW, kWh and What the Battery Actually Covers
kW is power; kWh is energy. Three-phase machinery with 3× inrush current is a kW problem: the bidirectional inverter has to be rated for that surge, which is why we specify a single industrial BESS rather than stacking single-phase units. The 900 kWh the plant uses in a day is a kWh problem: it sets the array size and the storage bank. Adding motor nameplate ratings together answers neither question.
Whole-site backup versus critical-load backup. Whole-site backup keeps every line running through an outage and needs a battery sized to full-shift power — typically two to three times the storage cost. Critical-load backup keeps only the line that cannot stop: the continuous process, the cold store, control and safety systems, and lighting. The deciding input is permitted downtime. A plant that can ride through 20 minutes needs far less battery than one that cannot lose a second, and that answer belongs in the specification before anyone prices the storage.
What We Need From You to Size a Factory System
Shift load — how many shifts, and the kW and kWh of each. Three-phase motor list — rating, quantity and starting method: direct-on-line, star-delta or variable-frequency drive. Critical production line — which line cannot stop, and what it draws. Permitted downtime — seconds, minutes, or until the end of the shift. Expansion allowance — whether a line is added in the next two to three years, so inverter and distribution capacity are reserved now. Roof condition — structure, orientation, usable area, and any corrosion, dust or heat that the equipment has to live with. We start from 7–14 days of logged consumption and split base load from shift peaks before anything is specified.
 English
 Arabic
 Spanish
 French
 Dutch
 Portuguese